Why Choose the Right Cutting Tool for Global Sourcing?
Global sourcing is not simply a search for the lowest cutting tool price. It is a decision about performance, consistency, delivery, and risk. A tool that looks economical on a quotation may create expensive problems on the shop floor. Excessive vibration, rapid wear, poor surface finish, and delayed replacements can quickly erase the original savings.
Dr. Tony Schmitz, a recognized machining researcher and professor, has emphasized this principle: “The tool-workpiece interface is where the process is decided.” His observation captures the practical importance of tool selection. Material grade, coating, geometry, machine rigidity, coolant method, and cutting parameters must work together. One carbide insert may perform well in stainless steel but fail quickly in hardened alloy. Small details matter.
Real sourcing decisions require evidence. Buyers should request test data, dimensional control records, coating information, and clear quality procedures. They should also examine technical support and replacement lead times. A reliable supplier can explain tool life with specific cutting conditions, not vague promises.
Price still matters.
But it is only one variable.
Experience teaches that even a respected supplier can deliver the wrong solution when specifications remain unclear. That weakness deserves attention. Global purchasing teams should compare total operating cost, not unit price alone. A controlled trial, measured tool life, and documented results can reduce uncertainty before larger orders begin. Choosing the right Cutting Tool protects production stability and supports more dependable international sourcing.
What Is a Cutting Tool and Why Does Its Selection Matter?
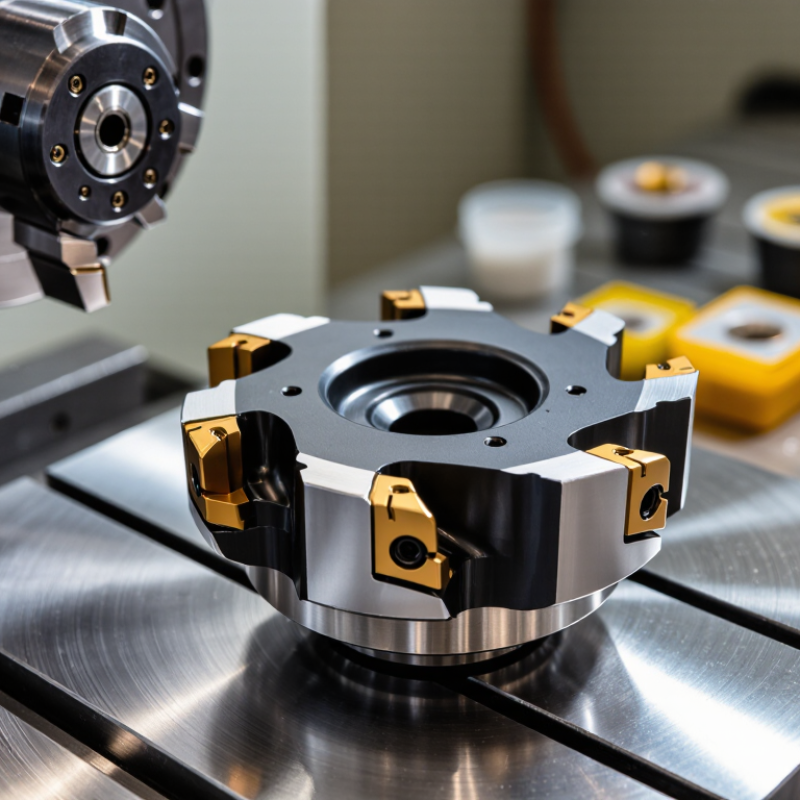
A cutting tool is a device that removes material from a workpiece. Drills, milling cutters, turning inserts, and saw blades are common examples. Each tool uses a specific edge shape, material, and cutting geometry. These details control cutting speed, surface finish, heat, and tool life. A small mismatch can create vibration, burrs, or early edge failure.
Selection matters because every production environment is different. Steel may need a tougher edge, while aluminum often benefits from sharper geometry. Machine power, spindle speed, coolant, and workholding also affect performance. I have seen a tool perform well in a test cell but struggle on an older machine. That result was not a tool defect. The operating conditions were different.
For global sourcing, buyers should request clear specifications, inspection records, and practical test data. Confirm diameter, tolerance, coating, substrate, and recommended cutting parameters. Packaging also matters when tools cross humid or long shipping routes. Traceable batches make quality problems easier to investigate. A trial order can reveal more than a polished catalog. Keep records of tool life, finished-surface quality, and replacement frequency. No selection is perfect. I have sometimes focused too heavily on purchase price and underestimated setup time. That mistake showed why total operating cost deserves equal attention. Reliable suppliers should answer technical questions clearly and provide consistent documentation.
How Material and Machining Conditions Determine Tool Requirements
Why Choose the Right Cutting Tool for Global Sourcing?
Material and machining conditions determine whether a cutting tool performs reliably. A tough stainless steel grade needs different geometry from soft aluminum. Hardened steel may require a stronger edge and heat-resistant coating. Tool selection should follow the material’s hardness, abrasiveness, and tendency to create built-up edges.
Machining conditions matter just as much. Cutting speed, feed rate, depth of cut, coolant delivery, and machine rigidity all affect tool life. During production trials, a tool may cut smoothly at low speed but fail quickly when the feed increases. I have also seen stable machines produce poor surfaces because chips were not leaving the cutting zone. That detail is easy to miss. It should not be.
Tips: Record the material grade, hardness, and batch condition. Confirm spindle power and holder accuracy. Test one controlled change at a time. A short trial often reveals more than a supplier’s general recommendation. Inspect chips, surface finish, tool wear, and cutting sound. These signs provide practical evidence before larger orders are placed. Do not rely only on catalog data; real machines rarely match ideal laboratory conditions. Keep a small record of successful settings for future sourcing decisions.
Which Cutting Tool Materials and Geometries Suit Global Production?
Why Choose the Right Cutting Tool for Global Sourcing?
Material choice affects tool life, supply stability, and machining consistency. ISO 513 classifies cutting materials by hardness, toughness, and thermal performance. Cemented carbide suits broad production because it balances wear resistance and impact strength. High-speed steel remains practical for interrupted cuts and lower-speed equipment. Ceramics handle heat well, but they need rigid machines and stable cutting conditions. CBN fits hardened steel, while PCD performs well on aluminum and abrasive composites.
Geometry matters as much as material. A positive rake angle can reduce cutting force in thin-wall aluminum parts. A stronger edge is safer for cast iron or interrupted cuts. Helix angle, corner radius, and chipbreaker design should match material behavior, not just machine power. The US Geological Survey’s Mineral Commodity Summaries 2024 reported about 81,000 metric tons of tungsten mine production in 2023. Much of the global supply remains concentrated in a few regions. That concentration can affect carbide costs and delivery schedules.
Global sourcing needs more than a low quoted price. Specify equivalent grades through ISO classifications, dimensional tolerances, and verified performance tests. Keep a second material option approved. It may prevent disruption. Still, standardization can become too rigid; one geometry rarely performs equally across every plant. A short trial using identical speeds, feeds, coolant, and workpiece batches gives better evidence than catalog claims. Small errors matter.
How Tool Quality Affects Cost, Productivity, and Product Consistency
Why Choose the Right Cutting Tool for Global Sourcing?
How Tool Quality Affects Cost, Productivity, and Product Consistency
Cutting tool quality directly influences sourcing costs, machining speed, and finished-part accuracy. A cheaper tool may appear attractive, but rapid wear can increase replacement, labor, and inspection expenses. Small details matter.
In production, I have seen tool geometry affect cycle time by several seconds per part. That difference becomes significant across thousands of components. Proper flute design, edge preparation, and coating selection should match the material and cutting conditions. A tool with stable runout also reduces vibration, surface marks, and unexpected scrap.
Consistency is measurable. Suppliers should provide tool specifications, tolerance data, test results, and clear batch-control procedures. Buyers can request sample trials using the intended material, spindle speed, feed rate, and coolant. These records make comparisons more reliable across countries and suppliers. Not every tool fits.
Cost per tool is an incomplete calculation. The better measure is cost per acceptable part, including downtime and rework. I once focused too heavily on tool price and underestimated setup delays. That decision looked efficient on paper, but production became less predictable. A stronger evaluation should combine tool life, cutting performance, delivery stability, and operator feedback. Even then, results may change between machines. Local testing remains necessary.
Why Choose the Right Cutting Tool for Global Sourcing?
How tool quality affects cost, productivity, and product consistency
The chart uses a brand-neutral manufacturing benchmark normalized to the Standard Tooling level at 100. Lower total cost and higher productivity and consistency indicate better sourcing performance. Higher-quality tools typically extend tool life, reduce changeovers and scrap, and help maintain tighter dimensional control.
What Should Buyers Evaluate When Sourcing Cutting Tools Internationally?
Why Choose the Right Cutting Tool for Global Sourcing?
What Should Buyers Evaluate When Sourcing Cutting Tools Internationally?
International buyers should evaluate more than unit price when selecting cutting tools. Tool performance depends on workpiece material, machine stability, cutting speed, and coolant conditions. A cutter designed for aluminum may fail quickly on hardened steel. Ask suppliers to state the recommended application range clearly.
Review the tool material, geometry, coating, diameter tolerance, and edge preparation. Request inspection records for critical dimensions. A reliable supplier should explain how tools are tested before shipment. Sample orders can reveal runout, surface finish, chip control, and actual tool life. Small details matter.
Check production capacity, quality systems, export packaging, and communication response times. Drawings, inspection reports, and material certificates should match the delivered tools. Confirm lead times in writing, including holidays and customs delays. Packaging must protect sharp edges from impact and moisture.
Do not trust impressive claims alone. Compare test conditions.
A lower price may reduce tool life, increase machine downtime, or create inconsistent parts. However, expensive tools are not automatically better. I have seen buyers over-specify coatings for simple applications, wasting budget without improving results. The better decision comes from controlled trials, measurable data, and honest feedback from operators. Leave room to revise the specification after real production testing.
Why Choose the Right Cutting Tool for Global Sourcing? - What Should Buyers Evaluate When Sourcing Cutting Tools Internationally?
| Evaluation Area | Measurable Specification | Typical Industry Data or Benchmark | Why It Matters in International Sourcing | Recommended Buyer Verification |
|---|---|---|---|---|
| Workpiece Material | Material grade, hardness, tensile strength, thermal conductivity | Common groups include steels, stainless steels, cast irons, non-ferrous alloys, hardened steels, superalloys and composites. | A tool suitable for one material group may wear rapidly or fail when used on another. | Request the supplier’s ISO material-group recommendation and test it against the buyer’s actual workpiece grade. |
| Tool Material | Carbide, cermet, ceramic, PCD or PCBN grade | Cemented carbide is widely used for general machining; PCD is commonly selected for abrasive non-ferrous materials; PCBN is used for many hardened-ferrous applications. | The substrate determines hardness, toughness, heat resistance and suitability for interrupted cuts. | Ask for grade composition, recommended workpiece materials and application limits rather than relying only on a product name. |
| Coating System | Coating type, coating process, layer structure and thickness | Common coating families include TiN, TiCN, TiAlN and Al2O3; performance depends on substrate, deposition method and cutting conditions. | Coatings can improve wear resistance, oxidation resistance and tool life, but no single coating is optimal for every material or coolant condition. | Request a technical data sheet identifying coating composition, application range and maximum recommended temperature or speed conditions. |
| Geometry and Edge Preparation | Rake angle, clearance angle, nose radius, edge hone and chip-breaker geometry | Positive geometries generally reduce cutting forces; stronger edge preparations are often used for interrupted cuts and harder materials. | Geometry affects power consumption, surface finish, chip control, vibration and edge reliability. | Confirm geometry drawings, dimensional tolerances and suitability for continuous, interrupted, roughing or finishing operations. |
| Dimensional Accuracy | Insert dimensions, shank diameter, cutting diameter, concentricity and tolerance class | Interchangeable inserts should match the relevant ISO designation and the toolholder’s seat, screw or clamping system. | Small dimensional differences can cause runout, poor surface finish, incorrect indexing or incompatibility with existing equipment. | Approve a dimensional drawing, first-article sample and inspection report before mass production. |
| Cutting Parameters | Cutting speed, feed per tooth or revolution, and depth of cut | Recommended values vary substantially by tool material, workpiece grade, machine rigidity, coolant and operation; supplier values should be treated as starting points, not universal limits. | Incorrect parameters can produce premature wear, thermal cracking, chatter or edge fracture. | Require parameter charts with units, workpiece materials, cutting method and test conditions clearly stated. |
| Tool Life | Minutes, parts, meters of cutting or allowable flank wear before replacement | Tool life should be compared only under identical workpiece, machine, coolant, cutting-parameter and wear-criteria conditions. | A lower purchase price may be uneconomical if tool changes, scrap and downtime are higher. | Use controlled trials and document tool life according to recognized methods such as ISO 3685 where applicable. |
| Surface Finish | Ra, Rz, dimensional deviation and burr formation | Surface roughness depends on feed, nose radius, tool condition, machine vibration and material behavior; theoretical turning roughness is often estimated from feed and nose radius but does not replace measurement. | Consistent finish is essential when tools are sourced from different countries or production sites. | Define acceptance limits and measure finished parts with calibrated instruments under documented conditions. |
| Machine Compatibility | Spindle speed, power, torque, holder interface, coolant delivery and machine rigidity | The tool must remain within the machine’s maximum speed, power, torque, travel and workholding limits. | A technically capable tool can still fail if the target machine cannot provide sufficient rigidity, speed or coolant flow. | Provide the supplier with machine specifications and request a machine-specific cutting recommendation. |
| Quality Control | Incoming inspection, batch traceability, hardness, coating adhesion and dimensional capability | ISO 9001 is a quality-management-system standard; certification does not by itself guarantee cutting performance. | Consistent inspection and traceability reduce variation between shipments and production batches. | Request current certificates, inspection plans, lot numbers, certificates of conformity and nonconformance procedures. |
| Total Cost of Ownership | Tool price, usable edges, tool life, setup time, freight, duties, scrap and downtime | Cost per part can be calculated as total tooling cost divided by acceptable parts produced, with setup and logistics costs included where material. | The lowest unit price does not necessarily provide the lowest production cost. | Compare suppliers using the same production quantity, performance target, delivery term and quality assumptions. |
| Packaging and Protection | Individual protection, moisture control, labeling, lot identification and transport packaging | Sharp cutting edges require protection against impact, corrosion, contamination and movement during transport. | International handling and longer transit times increase the risk of packaging-related damage. | Approve packaging samples and specify labeling, quantity per package, lot traceability and damage-claim procedures. |
| Lead Time and Supply Capacity | Sample lead time, standard production lead time, minimum order quantity and monthly capacity | Lead time varies by standard or special geometry, coating requirement, order quantity, inspection level and shipping method. | Unreliable replenishment can interrupt production even when tool performance is satisfactory. | Obtain written lead-time commitments, safety-stock recommendations, production-capacity evidence and escalation contacts. |
| Trade and Compliance Documents | Commercial invoice, packing list, certificate of origin, HS classification and applicable customs documents | Import requirements depend on the destination country, product classification, material composition and transaction value. | Incomplete or inaccurate documents can cause customs delays, unexpected duties or shipment holds. | Confirm documentation requirements with the buyer’s customs broker before placing the order. |
| Delivery Terms and Risk Allocation | Incoterms® rule, named place, insurance responsibility and transfer of risk | Incoterms® rules define selected buyer and seller responsibilities for delivery, costs and risk; they do not replace the sales contract. | Clear delivery terms prevent disputes over freight, insurance, customs clearance and damaged goods. | State the exact Incoterms® rule and named location in the purchase contract and commercial documents. |
| Technical Support | Application engineering, test reports, troubleshooting response time and replacement policy | Effective support should address tool selection, cutting parameters, failure analysis and corrective actions. | Remote sourcing increases the cost and time of resolving technical problems. | Include response-time targets, trial support, failure-analysis requirements and warranty or replacement terms in the supplier agreement. |
Note: Cutting data are application-dependent starting points. Final selection should be validated through controlled trials using the actual workpiece material, machine, holder, coolant and production requirements.
Related Posts
-
China Top 10 Cutting Tools Suppliers for Global Buyers
-
The Ultimate Guide to Choosing the Best Cutting Tools for Precision Cuts
-
Understanding the Importance of Cutting Tool Cutting in Modern Manufacturing Processes
-
Top Strategies for Choosing the Right Milling Cutter for Your Manufacturing Needs
-
Revolutionizing Global Procurement with Indexable Milling Cutters at the 137th Canton Fair
-
Challenges Faced in Achieving Optimal Results with Best Indexable Milling Techniques